BUYER'S GUIDE - 12 MIN READ
How to Verify PPE Supplier Production Capacity Before a Large Order
Editorial information, sources and corrections
Check PPE supplier capacity using product mix, bottlenecks, material readiness, staffing and order schedules rather than machine counts alone.
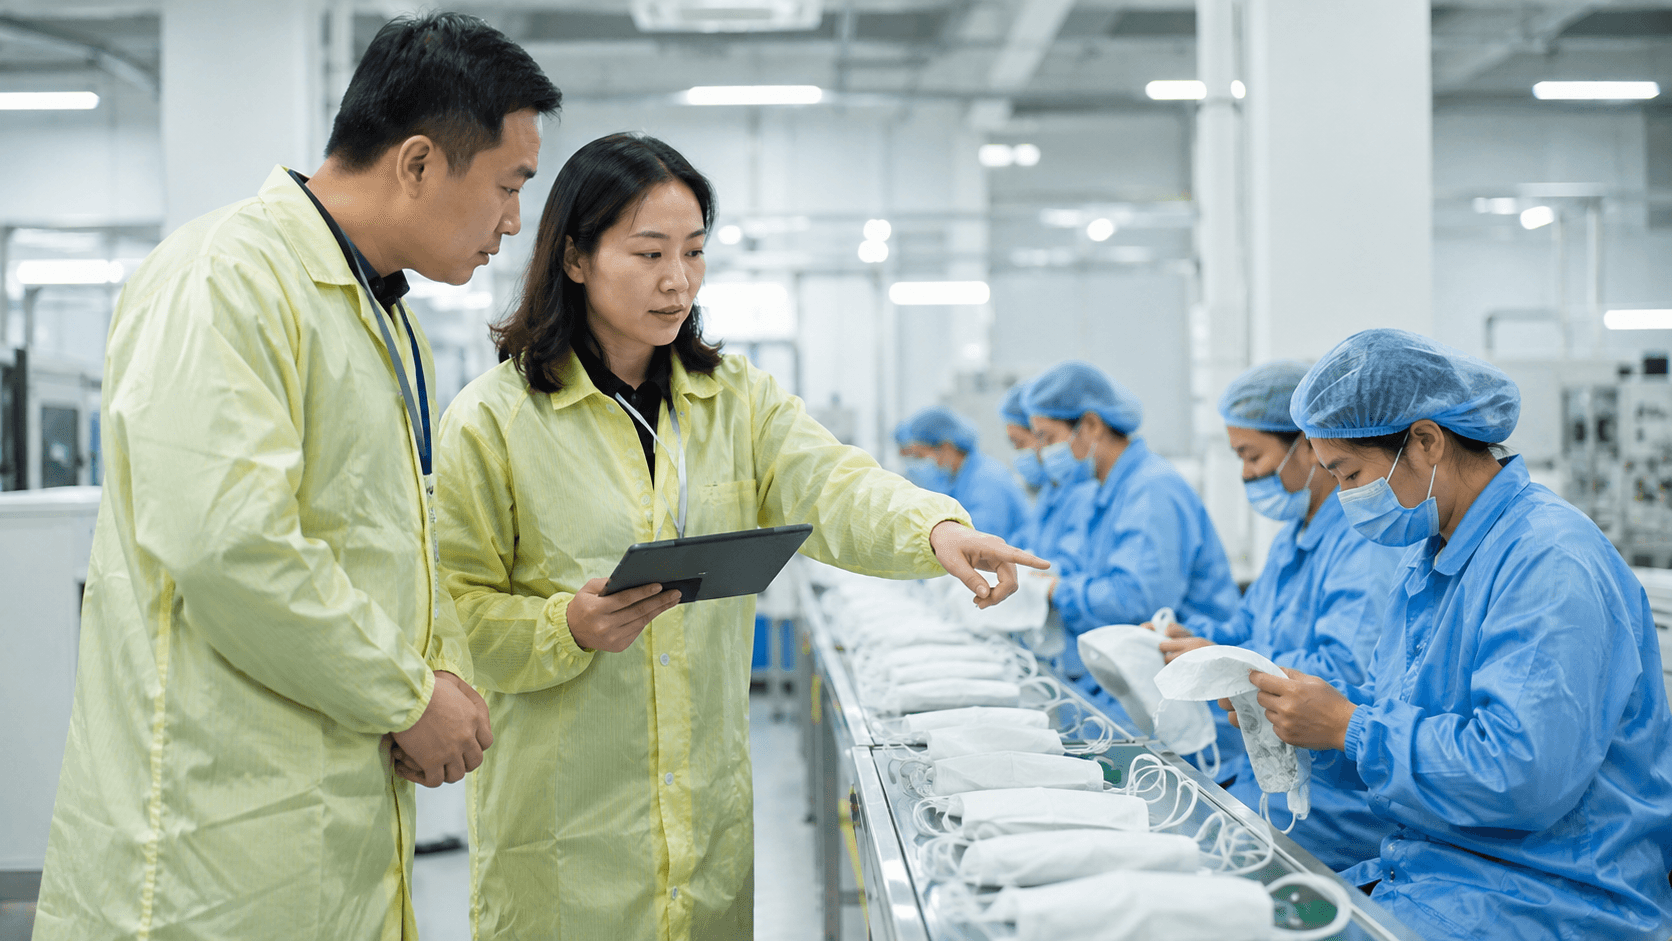
Illustrative image, not evidence of testing or a documented customer project. Procurement guidance does not replace product instructions or competent workplace assessment.
Primary topic: PPE supplier production capacity
Introduction
Quick answer: PPE supplier production capacity must be evaluated for the exact order mix and delivery window. Installed machines are not the same as available output. Connect material readiness, constrained operations, staffing, existing commitments, inspection and packing to a dated plan, then monitor evidence at the milestones most likely to affect shipment.
A supplier’s statement that it can make a million units per month is not yet a delivery commitment for your order. The figure may describe installed equipment, a best-case product, total output across several sites, or capacity already allocated to other customers.
Buyers should verify capacity for the exact product mix and delivery window. Review the process route, bottlenecks, available working time, material readiness, staffing, current commitments, quality losses, and packing capacity. Ask for evidence appropriate to the decision while respecting legitimate confidentiality.
This article proposes an operational assessment framework. It does not claim that a buyer can audit a factory fully from a spreadsheet or predict output with certainty.
Define the order in production terms
Translate the commercial request into model, size, color, construction, packaging, quantity, and required release dates. A factory cannot assess a meaningful load from “a large glove order” alone.
Identify differences that affect changeovers or process routes. Several sizes may share some operations but require different settings or packing. Private-label artwork can create additional preparation and inspection steps.
Distinguish production completion from shipment readiness. Goods may still require testing, inspection, labeling, packing, or document approval after the main manufacturing step.
State the buyer’s own dependencies. Late artwork approval or delayed sample decisions can affect the schedule. A capacity review should examine both sides of the process rather than treating every delay as a factory problem.
Map the actual process route
Ask which operations are performed at the proposed site and which are outsourced. The relevant capacity is the capacity of the complete route, not the most impressive machine in the presentation.
For a hypothetical glove program, the route might include material preparation, construction, coating where applicable, finishing, inspection, and packing. The exact route depends on the product and should come from the supplier.
Identify queues and transfers between stages. A fast production operation can feed a slow packing line, creating unfinished stock rather than dispatchable goods.
If subcontractors are involved, ask how their availability and quality controls enter the schedule. Do not assume outsourced work is either inherently unacceptable or automatically available.
Distinguish several meanings of capacity
Installed capacity describes equipment or theoretical capability. Demonstrated output reflects what has actually been achieved under stated conditions. Available capacity considers existing commitments. Committed capacity is what the supplier agrees to allocate to the order.
These figures should not be used interchangeably. A machine count may support an installed-capacity discussion but does not reveal staffing, maintenance, yield, or other orders.
| Capacity question | Evidence to discuss |
|---|---|
| What can the process theoretically do? | Equipment and process assumptions |
| What has it actually produced? | Relevant output records |
| What remains available? | Schedule and existing allocation |
| What is committed to this order? | Agreed plan and milestones |
Ask the supplier to label estimates and assumptions. An honest range with known constraints is more useful than a precise figure based on an unrelated product.
Find the bottleneck
The bottleneck is the operation that limits the relevant flow under the current conditions. It may change with the product mix. A finishing stage that is adequate for one model may constrain another.
Request a stage-by-stage view of planned output and work in progress. Large accumulation before one operation can indicate a constraint worth investigating.
Do not calculate overall capacity by adding output from sequential processes. If one stage produces 5,000 units and the next can finish 3,000, the completed flow is not 8,000.
Ask how the supplier handles variation, downtime, and rework. A schedule that assumes every hour is productive and every item passes first time may be unrealistic.
Review material readiness
Capacity is unusable without the right materials. Confirm which materials are in stock, allocated, ordered, or still awaiting approval. A general claim of raw-material availability should be tied to the actual construction.
Check supplier lead times for special colors, components, printed packaging, or customer-specific items. These can become critical even when the main production line is available.
Ask how material substitutions are controlled. A shortage should not lead to an unapproved change simply to preserve the shipment date.
The sample approval guide explains why the approved construction must remain connected to production. Capacity does not justify changing the product without review.
Send your PPE order schedule, including model mix, quantities, sizes, packaging, approval milestones, and required arrival dates. A meaningful capacity discussion starts with that detail.
Examine staffing and working-time assumptions
Ask which shifts and trained roles support the plan. Equipment availability is not enough if the relevant operators, inspectors, or maintenance support are unavailable.
Do not encourage unsafe working practices or unrealistic overtime as a solution. A sustainable schedule should account for applicable working arrangements and competent staffing.
Consider holidays, planned maintenance, training, and other known constraints. The buyer and supplier should discuss these openly before a date becomes a customer promise.
Where additional staffing is proposed, ask how training and quality control will be maintained. Rapid expansion can change the process risk even when it increases nominal labor hours.
Verify packing and inspection capacity
Finished goods can accumulate if packaging materials, label approvals, inspectors, or packing labor are unavailable. Treat these as part of the production plan, not minor afterthoughts.
Private-label and multi-destination orders may require more segregation and checks than standard packs. The schedule should reflect the actual configuration.
Agree when shipment inspection can occur and what proportion of the order must be complete under the chosen plan. Do not assume an inspector can validate unpacked or unidentified goods to the same scope as finished packs.
Use the shipment inspection checklist to define the release dependencies. A production completion date should not silently become a shipment date.
Request evidence proportionately
Useful evidence can include redacted output summaries, process schedules, material status, equipment records, and a live review of relevant operations. The depth should match order value, risk, and relationship history.
Respect other customers’ confidentiality. Ask for enough information to understand allocation without demanding unrelated customer names or commercial details.
Cross-check sources. A production schedule, material status report, and packing plan should tell a consistent story. Inconsistency is a reason to ask questions, not automatically proof of dishonesty.
For independent inspection or audit services, review competence and scope. ILAC’s accreditation overview offers general context on recognized conformity assessment activities; it does not make a supplier’s self-reported capacity independently verified.
Use milestones that reveal progress
Break the order into meaningful milestones: approved specification, material readiness, production start, defined output stages, packing completion, inspection, and release. Choose milestones appropriate to the product.
Ask for evidence linked to the order rather than generic daily factory photographs. A picture of active machinery may not show that your configuration is being produced.
Track exceptions and their effect on the critical path. A one-day delay in a noncritical activity may be recoverable; a delayed unique component may affect the entire schedule.
Do not reward optimistic reporting. A supplier should be able to flag a problem early without being pressured to maintain an unsupported date.
A hypothetical capacity review
A buyer requests 100,000 pairs of private-label gloves in several sizes. The supplier cites a monthly output far above that quantity. On closer review, the main manufacturing stage is available, but the required printed packaging has a longer lead time and the packing team is already committed.
The buyer and supplier revise the schedule around packaging and packing capacity. They consider an approved staged shipment, without changing the required product or destination information.
The final plan is more credible because it addresses the actual constraint. The original headline capacity figure was not necessarily false; it simply did not answer the buyer’s order-specific question.
This example is hypothetical and does not represent PPEgen production output.
Evaluate proposed recovery actions
If the plan slips, ask what specifically changes. Additional approved resources, revised sequencing, or a staged release may help. A vague promise to “speed up” does not explain how the bottleneck will be resolved.
Review the effect of any proposed production-site or material change. Recovery actions can create new technical, quality, or documentation requirements.
Keep customer communication realistic. Do not announce a recovered delivery date until the revised assumptions and dependencies have been checked.
Document the agreed action and next evidence point. This prevents repeated conversations that reset the promise without resolving the underlying problem.
Build an order-specific capacity worksheet
Ask the supplier to express the plan in a form tied to your configuration. The worksheet can list each major stage, planned start and finish, relevant quantity, available resources, dependencies, and evidence checkpoint. It need not expose other customers’ confidential details to be useful.
Separate the supplier’s estimate from a confirmed allocation. A planning discussion may begin with provisional assumptions, but the purchase commitment should identify which assumptions have been resolved and which remain conditional.
Test the arithmetic with a simple scenario
Suppose a hypothetical packing stage can complete 2,000 approved packs per working day under the stated staffing arrangement, and the order requires 20,000 packs. The nominal packing requirement is ten working days before considering interruptions or other commitments.
That arithmetic does not establish the actual schedule. The buyer still needs to know when goods and packaging reach the stage, whether those days are available, and how inspection or rework affects release. The example is a reasoning check, not a factory output benchmark.
Avoid adding parallel and sequential figures incorrectly
If two independent lines can genuinely produce the same approved configuration at the same time, their relevant available output may be combined in a plan. If operations are sequential, adding their output figures is misleading.
Ask the supplier to explain the flow when a capacity number seems unexpectedly large. The goal is to understand the basis, not to challenge every figure as suspicious.
Review the effect of product mix
An order with many sizes, colors, or packaging variants may require changeovers and additional identification controls. Request a schedule reflecting that mix rather than one based on continuous production of the easiest item.
If the buyer can simplify the mix without compromising requirements, discuss the commercial effect. Do not assume simplification is possible when sizes or destination versions serve necessary user needs.
Check recovery capacity separately
A schedule with no practical allowance for disruption may appear efficient but offer little resilience. Ask which approved actions are available if a stage falls behind and how quickly they can be implemented.
Do not count an unqualified subcontractor or unapproved material as recovery capacity. The proposed recovery must preserve the agreed product and evidence requirements.
At order close, compare planned milestones with actual results and identify the cause of differences. This creates a better basis for the next capacity discussion than either an optimistic brochure or a single late-delivery anecdote.
Review a proposed second production site
If the supplier offers another site to increase output, treat the change as more than a scheduling adjustment. Confirm the site's role, relevant process capability, product evidence implications, quality controls, and connection to the approved specification.
Do not assume that common ownership makes every site interchangeable. The responsible technical and quality reviewers should determine what verification is needed.
Ask how the two sites will identify their output and how records will remain traceable through packing and shipment. Mixed production without clear identity can make later investigation difficult.
Keep customer commitments aligned with evidence
Sales teams often need a delivery date before every production detail is final. Communicate the level of confidence and the remaining dependencies rather than presenting an estimate as a guarantee.
Use milestones to update that confidence. Material allocation, completed approval, and verified packing progress can reduce uncertainty, while an unresolved bottleneck should remain visible.
Do not change the meaning of the date during the project. Production completion, ready-for-inspection, dispatch, port arrival, and available-for-issue are different events.
Conduct an order-close review
Compare the original plan, approved changes, and actual milestones. Identify whether differences came from supplier execution, buyer approvals, materials, inspection, or logistics.
Use that evidence to improve the next plan. A supplier that reported a risk early and resolved it responsibly should not be judged only by the initial optimistic date, while repeated unexplained promises deserve attention.
Keep the review specific to the product and period. One successful order does not establish unlimited future capacity, and one delay does not explain every part of the supplier's operation.
This closes the loop between headline capability and demonstrated order performance.
Ask the supplier to identify the earliest point at which a delay would become unrecoverable under the approved plan. That information helps the buyer make timely decisions about customer communication or a qualified alternative. Waiting until the promised dispatch day can eliminate options that were available when the first constraint appeared.
FAQ
How should PPE manufacturing lead time be checked?
Break the lead time into approval, material, production, inspection, packing and dispatch stages. Identify which activities can overlap and which depend on a completed predecessor. A quoted number of days is difficult to evaluate unless the start condition and final milestone are clear to both buyer and supplier.
What does factory bottleneck analysis contribute to sourcing?
It identifies the operation that limits the relevant product flow under the proposed schedule. Review that stage's workload and constraints rather than averaging the speeds of every machine. A line may have unused equipment while one shared process prevents the order from reaching the promised completion date.
What proves PPE material readiness?
Ask for order-specific evidence appropriate to the stage, such as confirmed material availability and its approval status. Distinguish purchased, received and released material. A supplier saying that raw material is ordered does not establish that the correct approved input is physically ready for the scheduled production run.
Why should PPE packing capacity be reviewed separately?
Finished components still require correct sorting, labeling, inserts and carton preparation before dispatch. Mixed sizes or destination versions can create work not reflected in the main production figure. Confirm the resources and approved artwork for packing instead of assuming that production completion automatically means shipment readiness.
What should supplier capacity evidence distinguish?
Separate reported capability, available capacity, allocated order time and completed output. Identify which figures come from reviewed records or direct observation, and note uncertainties. Buyers should not present a supplier's broad marketing claim as an independently verified commitment for a particular model, quantity and delivery window.
Conclusion
Delivery planning must keep applicable product evidence separate from capacity claims; consult the European Commission PPE information. This reference supports the stated context, not certification of a PPEgen product.
Order-specific capacity is a chain of dependent resources and approvals, not a headline monthly number. Buyers should examine the full route and identify the actual constraint.
A credible supplier can explain assumptions, show relevant evidence, and communicate changes. That conversation is more valuable than an impressive factory photograph.
Discuss a bulk PPE production plan with your exact configuration and schedule. Review factory coordination capabilities and the supplier selection guide before finalizing the order.
BUYER RESOURCES
Continue your PPE sourcing research.
Explore relevant PPE categories and a primary safety reference alongside this guide.Use this source alongside destination-market requirements for the exact product and application.
READY TO DISCUSS YOUR REQUIREMENT?