BUYER'S GUIDE - 12 MIN READ
What Quality Checks Should Be Completed Before Purchasing or Receiving Safety Gloves?
Editorial information, sources and corrections
Plan safety glove quality checks from sample approval to receiving, covering identity, documents, dimensions, defects, sampling and controlled lot release.
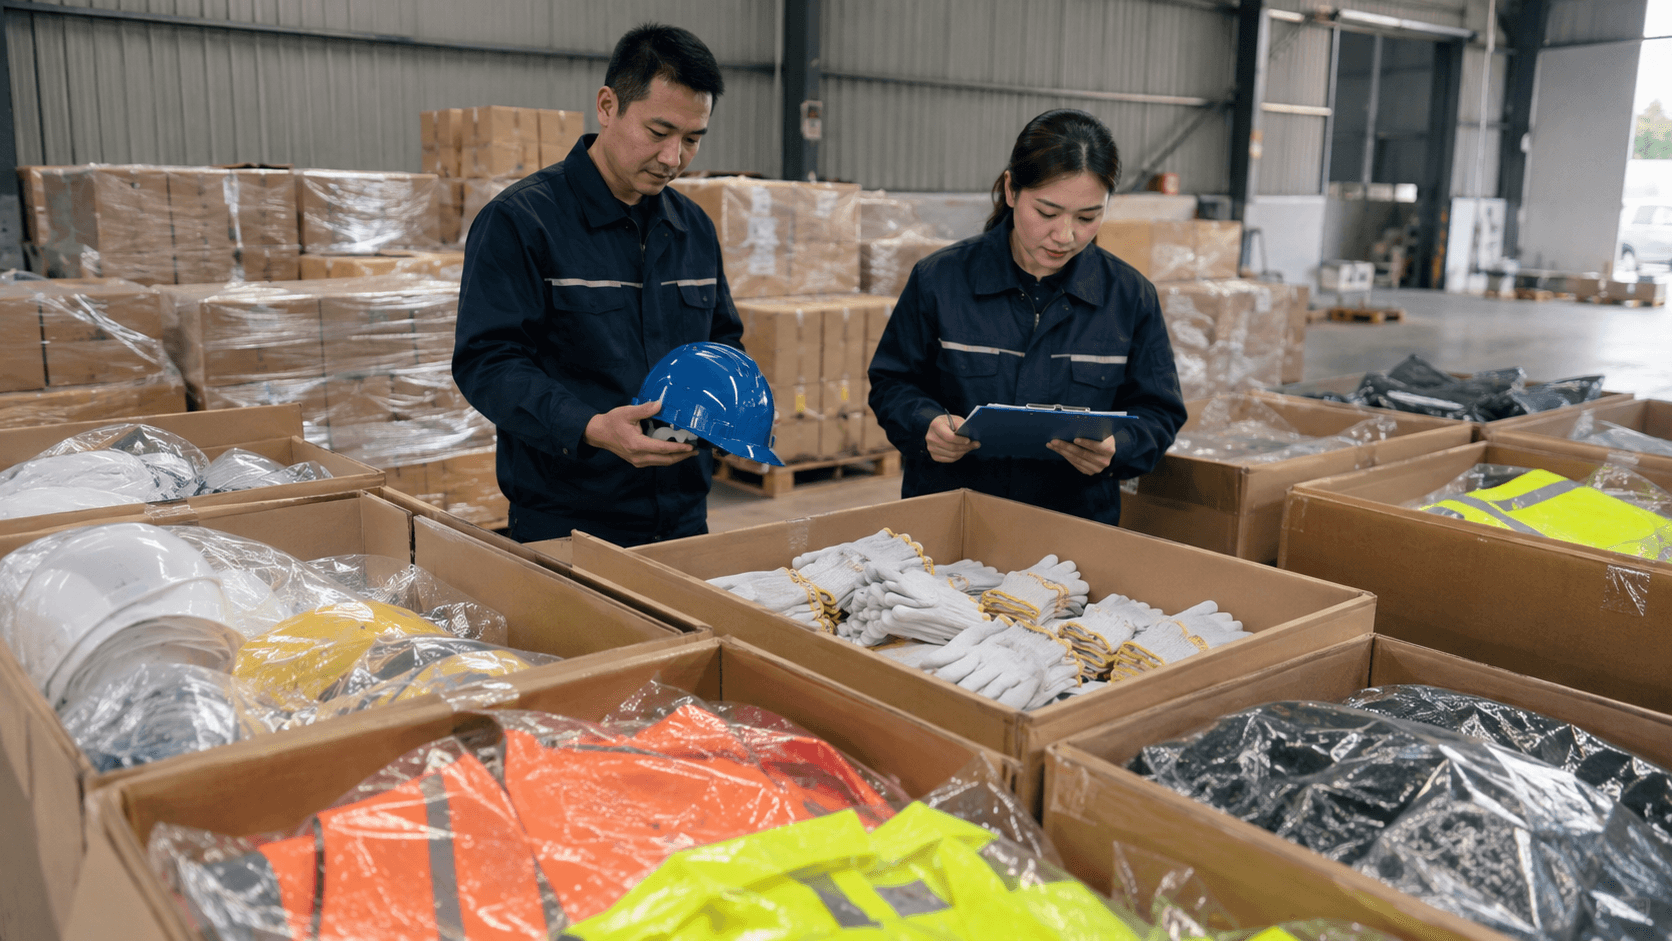
Illustrative image, not evidence of testing or a documented customer project. Procurement guidance does not replace product instructions or competent workplace assessment.
Primary topic: safety gloves quality inspection receiving checklist
Introduction
Before buying or receiving safety gloves, verify the product identity, relevant protective evidence, approved construction, dimensions, workmanship, markings, packing and lot traceability. Separate laboratory performance testing from shipment inspection and receiving checks. Each answers a different question; none should be described as a complete guarantee that every glove is suitable for every task.
A strong quality plan starts before the purchase order. The buyer and supplier need agreed specifications, inspection methods, defect definitions, sampling rules and a release authority. Waiting until cartons arrive makes disagreements harder to resolve because each side may be using a different understanding of acceptable. This guide explains a practical sequence for industrial glove purchasing, while leaving specialist tests and workplace suitability decisions with appropriately qualified reviewers.
Establish the approved reference first
Create a controlled specification for the exact model. Include the intended application, required protective properties, construction, sizes, relevant dimensions, markings, packaging and documentation. Record the revision and approval date. If a sample is retained, label it clearly and protect it from deterioration so it remains a useful reference.
A physical sample cannot communicate everything. It may show color and construction, but not the authenticity of a test report or the scope of a claimed rating. Pair the sample with a written specification and document index. Conversely, a written specification may not capture every workmanship detail, so reference photographs can clarify agreed appearance criteria.
Ask how production will be linked to the approved reference. An unchanged catalog name is not enough if the liner or coating can change. Define notification and approval requirements for relevant changes. This prevents the receiving inspector from discovering a substitution only after the shipment has already been paid for and distributed.
Verify documents against the exact glove
Match identity across the evidence
Compare the manufacturer, model, construction description, sizes and claimed performance on the data sheet, reports, instructions and supplied labels. Resolve discrepancies before approval. A report for a different model does not become applicable because the gloves look similar or are produced at the same factory.
Check what each document actually demonstrates. A management-system certificate concerns a management system; it does not establish every protective claim on an individual glove. A laboratory report concerns its stated sample and method. A declaration and any required conformity-assessment documents serve different roles. Keep these distinctions visible in the review record.
Confirm scope rather than collecting impressive paperwork
For EU-market products, consult the European Commission's PPE guidance when checking the applicable framework. Its warning about misleading voluntary certificates is particularly relevant to sourcing. The buyer should verify the appropriate route and model linkage, not count the number of certificates attached to an email.
Our safety glove standards and markings guide addresses this document review in more detail. The quality plan should record who completed the review, unresolved questions and the conditions under which the product can proceed to sample evaluation.
Inspect samples for construction and consistency
Examine the liner, coating coverage, fingertip formation, thumb area, seams where present and cuff construction. Compare the sample with the specification and check for obvious damage, incomplete coverage where coverage is required, loose components or foreign material. Do not invent universal cosmetic tolerances; agree criteria appropriate to the actual product and use.
Measure the specified dimensions using a defined method. State whether the glove is laid flat, relaxed or measured in another specified condition. Different handling can produce different results on a flexible product. Use suitable measuring equipment and record actual values rather than simply writing size correct.
Check more than one size where the order includes a range. A satisfactory medium sample does not establish that the smallest and largest sizes fit or match the specification. Record the sample quantity and origin, recognizing that supplier-selected development samples do not necessarily represent the eventual production lot.
Keep fit evaluation separate from protective testing
Use a controlled fitting exercise to assess finger length, palm fit, cuff behavior and permitted handling movements. Record participant size information and the model tried. A poor fit should trigger a sizing or model review, not an informal alteration to make the sample pass.
Do not cut, puncture, heat or chemically expose gloves while someone is wearing them to demonstrate protection. Such demonstrations are unsafe and do not substitute for the applicable test method. Formal performance claims require appropriate evidence from the relevant testing and conformity process.
A wearer trial can identify practical issues such as difficulty releasing a blunt sample object or a cuff that shifts during movement. Describe those observations accurately. Do not turn a favorable trial into a claim that the glove has passed a new protection test or is suitable for hazards not included in the original assessment.
Define the production inspection plan
The plan should identify the lot, inspection stage, sampling method, characteristics checked, defect classifications and acceptance rules. Agree it before production begins. A statement such as standard AQL inspection is incomplete unless the parties know which procedure, inspection level, limits and switching arrangements apply where relevant.
ISO's introduction to the ISO 2859 sampling series describes a family of attribute-sampling systems. Select an appropriate current procedure with a competent quality professional rather than copying a sample size from an unrelated order. Sampling supports a defined lot decision; it is not a promise that no defective unit exists.
Separate critical concerns from cosmetic preferences
Agree which conditions require immediate escalation and which are evaluated under the chosen acceptance plan. A missing protective component or an identity mismatch should not disappear inside a general appearance score. At the same time, an insignificant shade difference should not be described as a proven safety failure without a technical basis.
Photographs and examples help inspectors apply consistent definitions. Include ambiguous cases in the agreement so the supplier and buyer can resolve them before a disputed shipment. Record actual observations and quantities, not only a final pass or fail label.
Use an inspection matrix tied to decisions
| Inspection area | Example checks | What the result supports |
|---|---|---|
| Identity | Model, size, lot, manufacturer information | Whether the supplied item matches the order |
| Construction | Liner, coating, seams, cuff and components | Conformance to the approved specification |
| Dimensions | Agreed locations and measurement method | Size consistency against stated tolerances |
| Markings | Required content, legibility and model linkage | Correct identification and communication |
| Packing | Quantity, size mix, inner packs and carton condition | Delivery accuracy and handling suitability |
| Performance evidence | Relevant reports and agreed verification tests | Support for specific protective claims |
The final column matters because buyers sometimes ask a visual inspector to certify properties that cannot be established visually. Define the boundary of each check and arrange additional evidence where the risk requires it. A good inspection report is clear about limitations as well as findings.
Send Your Requirements to PPEgen with your specification, destination, size mix and proposed inspection plan. Request the model documentation and inspection arrangements needed for your own approval and release process.
Plan factory testing without confusing it with shipment inspection
Factory testing can refer to many activities, from routine process checks to a defined performance test. Ask exactly what is tested, by which method, how often, on which samples and how the result is recorded. The phrase tested in our factory is not a complete description of evidence.
Where an independent laboratory test is required, define sample selection and traceability before dispatching samples. Record whether the samples came from development stock or the actual production lot. Keep laboratory correspondence and reports linked to the purchase order and model revision.
Shipment inspection normally examines the consignment against agreed requirements at a particular stage. It may verify quantity, workmanship, markings and packing, but does not automatically repeat every protective test. Make these limitations explicit so a passed inspection is not later marketed as a broader certification.
Check the shipment when it arrives
Receiving inspection begins with the delivery identity and carton condition. Compare the purchase order, packing list, shipment references and quantities. Record visible transport damage before moving affected stock into normal storage. Photographs should show enough context to connect the issue to the shipment without exposing unnecessary personal or commercial information.
Verify the actual model, sizes, lots and pack counts according to the receiving plan. Do not assume that a pre-shipment report makes all arrival checks unnecessary; transport, handling or picking errors can occur after inspection. Conversely, receiving staff should not improvise technical tests beyond their training and authority.
Keep goods awaiting review physically or electronically separated from released stock. If a document is missing or an identity mismatch appears, define a hold decision and escalation route. The pressure to supply a department should not convert an unresolved issue into an undocumented release.
Handle nonconformities with traceable decisions
Record the issue, affected lot, observed quantity, evidence and immediate action. Ask the supplier for an explanation and proposed correction, but keep release authority with the designated buyer-side role. A verbal assurance that the difference is normal is not enough to close a documented mismatch.
Possible outcomes include clarification, sorting, replacement, rework where appropriate or rejection. Each needs defined criteria and verification. Do not accept a concession that changes the required protective suitability without technical approval. Commercial compensation does not make an unsuitable glove appropriate for use.
When only part of a delivery is affected, preserve lot segregation and the rationale for any partial release. Avoid mixing questionable and accepted stock during sorting. Record how the final decision was communicated to the warehouse and the users so the status remains clear after the inspection team leaves.
A hypothetical receiving discrepancy
Imagine an importer receives the correct carton count, but a sample of opened cartons contains a different cuff marking from the approved reference. The receiving team does not immediately assume counterfeit goods or ignore the difference as printing variation. It holds the affected lot and compares the model, production records and approved artwork.
The supplier explains whether the change is merely an approved label revision or signals a different product. The buyer's responsible reviewer assesses the evidence and determines the next action. If identity cannot be established, the stock remains unreleased. This example is a decision scenario, not a reported PPEgen shipment or claim about a particular supplier.
The useful lesson is that a small visible difference can require a document check rather than an improvised physical test. Equally, a plausible explanation must be supported by records. Quality control works when observations lead to a clear, traceable decision.
Preserve records for repeat orders and complaints
Keep the approved specification, sample reference, reports, inspection findings, release decision and shipment details together. Define a retention approach consistent with applicable obligations and business needs. A future complaint is easier to investigate when the company can identify which model revision and lot reached the customer.
Review recurring defects and disagreements before the next order. If inspectors repeatedly debate the same cosmetic feature, improve the specification. If production repeatedly differs from the approved construction, investigate change control rather than merely increasing inspection photographs. Inspection can detect some problems, but clear requirements and controlled production are needed to prevent recurrence.
Link the quality file to the bulk glove importer checklist. Technical acceptance, import documentation and warehouse release are connected, but they remain distinct responsibilities that should each have a named owner.
Make the inspection record usable by another reviewer
A useful report allows someone who was not present to understand the decision. Include the lot identification, inspection date, sample-selection approach, specification revision, actual findings and photographs tied to the finding numbers. State which checks were not performed and why. A folder of unlabeled images cannot reliably show whether an issue occurred in one sample or across several cartons.
Where measurements are taken, retain the units, method and instrument identification appropriate to the quality plan. Flexible gloves can be positioned differently, so a disputed dimension may require checking the measurement method before concluding that production changed. Do not average away an individual nonconformity where the agreed acceptance rule treats individual results separately.
The release record should name the authorized decision-maker and any conditions attached to acceptance. If a corrective action remains open but does not prevent release under the approved plan, explain that distinction. If release is prohibited pending evidence, make the hold visible to the warehouse. This administrative clarity is not a replacement for technical quality; it is what allows technical findings to influence the actual movement of stock. Without it, a careful inspection can be undermined by an accidental pick from the wrong pallet.
FAQ
Does a passed shipment inspection prove every glove is defect-free?
No. A sampling inspection supports the lot decision defined by its procedure and scope. It does not examine every property of every item. The report should state what was checked, how samples were selected and what limitations remain.
Can visual inspection confirm a cut-resistance rating?
No. Appearance and workmanship checks cannot establish a laboratory protection classification. Obtain relevant model-linked evidence and any agreed verification testing. Never attempt to demonstrate cut protection by applying a blade to a glove being worn.
Should buyers inspect every size?
The plan should address the actual size range and associated risks. One sample size may not reveal dimensional or packing issues in others. Agree sampling and coverage with the responsible quality professional rather than assuming a universal rule for every order.
What happens when the supplied label differs from the sample?
Hold the affected stock as appropriate and investigate the difference against approved documents. It may be an authorized revision or a significant identity problem. Record the evidence and decision before release; do not rely on an undocumented verbal explanation.
What should a pre-purchase quality request contain?
Send the model specification, application, required evidence, size schedule, packing requirements and proposed inspection criteria. Identify who approves samples and who releases production lots. Clear responsibilities make the supplier's response more useful and reduce disputes at delivery.
Conclusion
Safety glove quality checks should connect the approved requirement to the product actually delivered. Verify documents and samples first, define production and shipment checks, inspect arrivals and hold unresolved stock until an authorized decision is made. Clear boundaries between performance testing, visual inspection and workplace suitability make the resulting evidence more trustworthy.
Contact Us or email info@ppegen.com with your glove specification and inspection expectations. PPEgen can discuss sourcing documentation and quality-control arrangements without replacing your independent technical approval process.
BUYER RESOURCES
Continue your PPE sourcing research.
Explore relevant PPE categories and a primary safety reference alongside this guide.Use this source alongside destination-market requirements for the exact product and application.
READY TO DISCUSS YOUR REQUIREMENT?